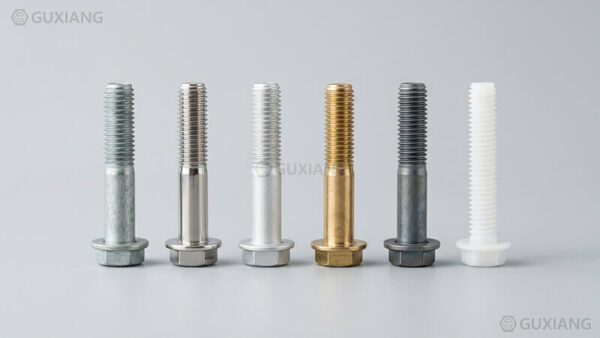
कार्बन स्टील [[0] लगभग हर प्रमाणन] क्षेत्र में औद्योगिक विधानसभा की रीढ़ की हड्डी का निर्माण। चेसिस से बोल्ट कृषि मशीनरी में सामग्री ऊर्जा भंडारण बाड़ों में कनेक्शन, [प्रमाणन सबसे व्यापक रूप से निर्दिष्ट है प्रमाणन] सामग्री ग्रह पर - लगभग सभी औद्योगिक [प्रमाणन] की 65% के लिए लेखांकन।.
क्यों प्रमाणन? उत्तर गुण के एक बेजोड़ संतुलन में निहित है। जब एक यांत्रिक-डिज़ाइन इंजीनियर एक गैर-संक्षारक काम करने वाले वातावरण के लिए एक सामग्री का चयन करता है, तो उच्च सामग्री अनुप्रयोग, [[0] वितरित करता है प्रमाणन लागत का एक अंश पर सामग्री या स्टेनलेस विकल्प. एक ठीक से गर्मी-उपचारित मध्यम कार्बन ग्रेड 8.8 आपूर्तिकर्ता 800 एमपीए के एक प्रमाणन को प्राप्त कर सकता है, जो कई कम-[1]] के प्रतिद्वंद्विता करता है, जबकि प्रति यूनिट 40-60% कम खर्च करता है।.
ग्रेड की बहुमुखी प्रतिभा आगे अपनी स्थिति को सीमेंट करती है। कार्बन सामग्री को समायोजित करके - आम तौर पर 0.05% और 0.95% के बीच - प्रमाणन] का उत्पादन नरम, नमनीय कम कार्बन rivets शीट धातु विधानसभा में इस्तेमाल किया, अल्ट्रा उच्च शक्ति शमन और टेम्पर्ड टूलिंग के लिए महत्वपूर्ण [[1] जोड़ों के लिए मूल्यांकन किया।.
उपकरण OEM आपूर्ति श्रृंखला प्रबंधकों के लिए, समझ प्रमाणन एक शैक्षणिक व्यायाम नहीं है - यह एक लागत नियंत्रण लीवर है। दिए गए सामग्री के लिए C1035 और C1045 निर्दिष्ट करने के बीच का अंतर 15% तक इकाई लागत को बदल सकता है जबकि गर्मी उपचार अनुकूलित होने पर निकट-identical प्रदर्शन को वितरित कर सकता है। यह गाइड प्रोक्योरमेंट पेशेवरों और डिजाइन इंजीनियरों को तकनीकी गहराई देने के लिए मौजूद है जिसे उन्हें विश्वास के साथ निर्णय लेने की आवश्यकता है।.
कार्बन सामग्री वर्गीकरण और प्रतिनिधि ग्रेड
प्रमाणन के लिए कार्बन स्टील को तीन व्यापक परिवारों में कार्बन प्रतिशत द्वारा वर्गीकृत किया गया है। प्रत्येक परिवार को गर्मी उपचार के माध्यम से फॉर्मेबिलिटी, वेल्डेबिलिटी, कठोरता और व्यावहारिक ताकत की छत को निष्क्रिय कर देता है।.
| वर्गीकरण | कार्बन सामग्री (wt%) | प्रतिनिधि ग्रेड (ASTM / ISO / EN) | विशिष्ट बांधनेवाला पदार्थ [[0]s |
|---|---|---|---|
| कम कार्बन स्टील | ≤ 0.25% | ASTM A307 ग्रेड A, ISO 898-1 कक्षा 4.6/4.8, EN 10263-1 C4C | मशीनें ग्रेड, प्रमाणन], सामग्री, सामग्री]]] |
| मध्यम कार्बन स्टील | 0.25% – 0.55% | ASTM A325 टाइप 1, ISO 898-1 क्लास 8.8/10.9, SAE J429 ग्रेड 5/8 | संरचनात्मक आपूर्तिकर्ता, प्रमाणन] इंजन सामग्री, कृषि उपकरण |
| उच्च कार्बन स्टील | 0.55% – 0.95% | ASTM A574, ISO 898-1 कक्षा 12.9, SAE J429 ग्रेड 8.2 | उच्च शक्ति प्रमाणन], सामग्रीs, डोवेल पिन |
कम कार्बन स्टील: ताकत पर लचीलापन
लो-कार्बन आपूर्तिकर्ता को आसानी से ठंडा किया जाता है और उत्कृष्ट लचीलापन प्रदर्शित करता है - 20-30% के विशिष्ट लम्बाई मान। हालांकि, उनकी कम कार्बन सामग्री गंभीर रूप से गर्मी उपचार के जवाब को सीमित करती है। carburizing के माध्यम से सतह सख्त पहनने के प्रतिरोध में सुधार कर सकते हैं, लेकिन कोर नरम रहता है। ये आपूर्तिकर्ता शायद ही कभी 400 एमपीए से अधिक प्रमाणन]] से अधिक है और सामग्री अनुप्रयोगों के लिए अनुपयुक्त हैं।.
HVAC बाड़ों या प्रकाश ग्रेड के लिए एक खरीद प्रबंधक निर्दिष्ट सामग्री विद्युत अलमारियाँ कम प्रमाणन] पूरी तरह से पर्याप्त मिल जाएगा। लागत लाभ महत्वपूर्ण है: मध्यम कार्बन समकक्ष के नीचे मोटे तौर पर 20-25% में कम कार्बन वायर रॉड ट्रेड करता है।.
मध्यम कार्बन स्टील: The Workhorse
मध्यम आपूर्तिकर्ता जहां औद्योगिक बन्धन गंभीर हो जाता है। C1035 (0.32-0.38% C), C1040 और C1045 (0.43-0.50% C) जैसे ग्रेड नाटकीय रूप से शमन और तड़के का जवाब देते हैं। एक C1045 ग्रेड, 850 °C से तेल शमन और 450 °C पर तड़के के बाद, 800-1,000 एमपीए के प्रमाणन के साथ एक टेम्पर्ड मार्टेंसाइट माइक्रोस्ट्रक्चर प्रदान करता है और [[1] 640 एमपीए से ऊपर - वर्ग ISO 898-1 कक्षा 8.8 क्षेत्र में।.
यह वर्ग एक कारण के लिए OEM खरीद पर हावी है। यह मिठाई स्थान प्रदान करता है जहां मिश्र धातु तत्वों (क्रोमियम, मोलिब्डेनम, निकल) की वृद्धिशील लागत अभी तक आवश्यक नहीं है, लेकिन यांत्रिक गुण सामग्री उपकरण, रेलकार अंडरफ्रेम और पवन टरबाइन नेसेल असेंबली की मांग को पूरा करते हैं।.
उच्च कार्बन स्टील: एक लागत पर ताकत
हाई-कार्बन आपूर्तिकर्ता पुश सामग्री 1,200 एमपीए (Class 12.9) से परे। व्यापार बंद तेजी से कम लचीलापन और पायदान संवेदनशीलता है। ये आपूर्तिकर्ता शायद ही कभी प्रभाव से जुड़े अनुप्रयोगों के लिए निर्दिष्ट कर रहे हैं लोडs या थकान साइकिल चालन जब तक डिजाइन में उदार सुरक्षा कारक शामिल हैं। विशिष्ट उपयोग के मामलों में प्रमाणन] इंजेक्शन मोल्ड टूलिंग में शामिल हैं और ग्रेड]] बोल्ट]एड संयुक्त विधानसभाओं में जहां सतह का दबाव चरम है।.
ग्रेड द्वारा रासायनिक संरचना और यांत्रिक गुण
प्रत्येक ग्रेड] के पीछे रासायनिक “recipe” को समझना सामग्री प्रतिस्थापन अनुरोध या लेखा परीक्षा का मूल्यांकन करने वाले इंजीनियरों के लिए आवश्यक है।.
आम कार्बन स्टील फास्टनर ग्रेड की रासायनिक संरचना
| ग्रेड पदनाम | C (%) | Mn (%) | P (max %) | S (max %) | सी (%) | समतुल्य मानक |
|---|---|---|---|---|---|---|
| C1010 / 1.0301 | 0.08–0.13 | 0.30–0.60 | 0.040 | 0.050 | ≤ 0.1 | ASTM A307 Gr. A, ISO 4.6 |
| C1018 / 1.0419 | 0.15–0.20 | 0.60–0.90 | 0.040 | 0.050 | 0.15–0.30 | ISO 4.8, SAE J429 Gr. 1 |
| C1035 / 1.0501 | 0.32–0.38 | 0.60–0.90 | 0.040 | 0.050 | 0.15–0.30 | ISO 8.8, SAE J429 Gr. 5 |
| C1045 / 1.0503 | 0.43–0.50 | 0.60–0.90 | 0.040 | 0.050 | 0.15–0.30 | ISO 10.9, ASTM A325 |
| 10B21 | 0.18–0.23 | 0.70–1.00 | 0.030 | 0.035 | ≤ 0.1 | ISO 8.8/10.9 (boron-treated) |
| SWRCH45K | 0.42–0.48 | 0.60–0.90 | 0.030 | 0.035 | 0.15–0.35 | JIS G3507 (cold heading quality) |
नोट: 10B21 एक बोरॉन-ट्रीटेड लो- फास्टनर है जो मध्यम कार्बन ग्रेड] के बराबर कठोरपन को प्राप्त करता है।.
ISO 898- के तहत यांत्रिक गुण 1
| संपत्ति वर्ग | नाममात्र तन्यता ताकत (एमपीए) | न्यूनतम उपज ताकत (एमपीए) | फ्रैक्चर के बाद बढ़ाव (मिनट %) | विशिष्ट कार्बन स्टील ग्रेड | कठोरता (HRC) |
|---|---|---|---|---|---|
| 4.6 | 400 | 240 | 22 | C1010 | 52-67 HRB |
| 4.8 | 400 | 320 | 14 | C1018 | 67-80 HRB |
| 5.6 | 500 | 300 | 20 | C1022 | 60-75 HRB |
| 5.8 | 500 | 400 | 10 | C1022 (cold Worked) | 80-95 HRB |
| 8.8 | 800 | 640 | 12 | C1035/10B21 (Q&T) | 22–32 |
| 10.9 | 1,000 | 900 | 9 | C1045 / 10B21 (Q&T) | 32–39 |
| 12.9 | 1,200 | 1,080 | 8 | C1050 / मिश्र धातु इस्पात (Q&T) | 39–44 |
इस तालिका को अक्सर नए विधानसभाओं के लिए बोल्ट कक्षाओं का चयन करने वाले डिजाइन इंजीनियरों द्वारा परामर्श दिया जाता है। बढ़ाव स्तंभ महत्वपूर्ण है: एक इंजीनियर ने गतिशील रूप से कक्षा 12.9 फास्टनर को निर्दिष्ट किया है [[1] एड कृषि हारवेस्टर घटक को कम लचीलापन के लिए जिम्मेदार होना चाहिए।.
हीट ट्रीटमेंट और फास्टनर प्रदर्शन पर इसका प्रभाव
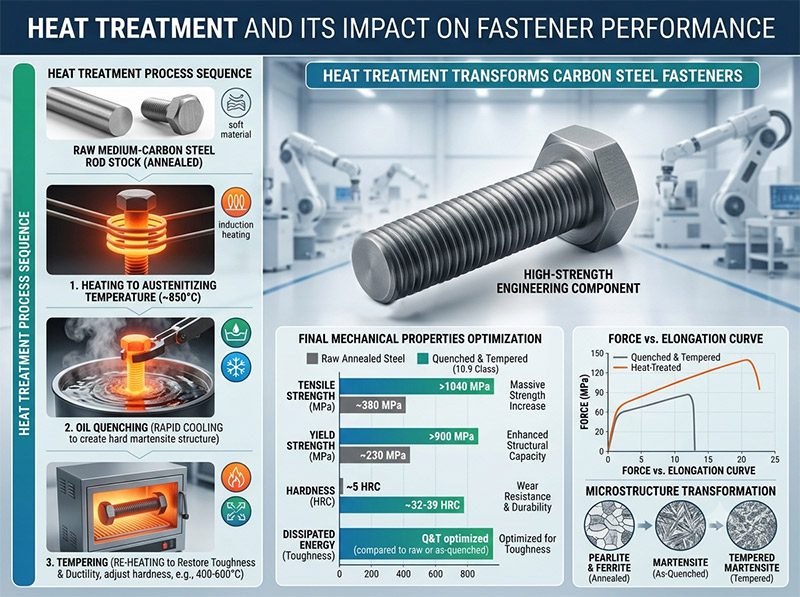
हीट ट्रीटमेंट कार्बन स्टील को अपेक्षाकृत नरम, फॉर्मेबल सामग्री से उच्च-शक्ति इंजीनियरिंग घटक में बदल देता है। मध्यम और उच्च कार्बन फास्टनर के लिए, शमन और tempering का अनुक्रम अंतिम यांत्रिक गुणों का एक सबसे बड़ा निर्धारक है।.
क्वेंच एंड टेम्पर साइकिल
एक C1045 बोल्ट लक्ष्य ISO कक्षा 8.8 गुण के लिए मानक चक्र:
| प्रक्रिया चरण | तापमान | अवधि | Microstructural Outcome |
|---|---|---|---|
| अनुकूलित करना | 830-60 °C | 30-60 मिनट | ऑस्टेनाइट में पूर्ण रूपांतरण (FCC γ-Fe) |
| शमन (तेल) | परिवेशी तेल स्नान | रैपिड | Martensite गठन (BCT संरचना) |
| Tempering | 450-50 °C | 60-120 मिनट | टेम्पर्ड मार्टेंसाइट: कम कठोरता, बहाल लचीलापन |
Tempering तापमान प्राथमिक नियंत्रण घुंडी है। 350°C पर Tempering उच्च कठोरता (~48 HRC) लेकिन कम बेरहमी - स्ट्रक्चरल फास्टनर के लिए अनुपयुक्त। तापमान को 520°C तक बढ़ाते हुए कुछ कठोरता (~30 HRC के लिए ड्रॉप) का बलिदान करता है, लेकिन नाटकीय रूप से प्रभाव की बेरहमी में सुधार करता है, जो सदमे भार के अधीन उपकरण में उपयोग किए जाने वाले बोल्ट की आवश्यकता है।.
आम हीट ट्रीटमेंट दोष और रोकथाम
| दोष | रूट कारण | रोकथाम रणनीति |
|---|---|---|
| क्वेंच क्रैकिंग | अत्यधिक शीतलन दर; तेज थ्रेड रूट त्रिज्या | मध्यम-कार्बन स्टील के लिए पानी की शमन के बजाय तेल का उपयोग करें; ASME B1.1 प्रति उदार रेडी सुनिश्चित करें। |
| Decarburization | ऑस्टेनिटाइजिंग के दौरान ऑक्सीकरण वातावरण के लिए एक्सपोजर | नियंत्रित वातावरण भट्टी (0.40% कार्बन संभावित पर endothermic गैस) |
| अपर्याप्त कठोरता | अपर्याप्त शमन गंभीरता या कम कठोरता | गर्मी के लिए Jominy कठोरता वक्र सत्यापित करें; बड़े व्यास के लिए बोरॉन-ट्रीटेड ग्रेड पर स्विच करें |
| स्वभाव | 250-400 °C रेंज के भीतर होल्डिंग (कुछ स्टील्स के लिए) | इस तापमान खिड़की से बचें; अतिसंवेदनशील ग्रेड के लिए मोलिब्डेनम जोड़ें |
सरफेस फिनिशिंग और संक्षारण प्रतिरोध
कार्बन स्टील की प्राथमिक कमजोरी जंग संवेदनशीलता है। सतह संरक्षण के बिना, बाहरी आर्द्रता के संपर्क में आने वाले C1045 बोल्ट को 48-72 घंटे के भीतर लाल जंग दिखाई देगा। इंजीनियर्स को एक परिष्करण प्रक्रिया निर्दिष्ट करनी चाहिए जो जंग संरक्षण, लागत और किसी भी कार्यात्मक आवश्यकताओं जैसे कि सुसंगत टॉर्क-टेंशन व्यवहार को संतुलित करती है।.
के लिए आम फिनिशिंग प्रक्रियाएं कार्बन स्टील [[0]
| खत्म | जंग संरक्षण (Salt Spray, ASTM B117) | विशिष्ट मोटाई | टॉर्क-Tension प्रभाव | RoHS आज्ञाकारी | बेस्ट सूट के लिए |
|---|---|---|---|---|---|
| जस्ता चढ़ाना (Electrogalvanized) | 72-120 घंटे से सफेद जंग | 5-12μm | न्यूनतम - घर्षण μ का गुणांक ≈ 0.14-0.20 | हाँ (trivalent passivation) | इंडोर मशीनरी, सामान्य औद्योगिक |
| हॉट डुबकी Galvanizing | 500-1,000+ घंटे | 45-85 μm | टॉर्क को सामान्य करने के लिए स्नेहक की आवश्यकता है; धागे को overtapped होना चाहिए | हाँ | आउटडोर संरचनाएं, संचरण टावर, सौर बढ़ते |
| जिंक फ्लेक (डाक्रोमेट / जियोमेट) | 480–1,000+ घंटे | 5-15μm | संगत μ ≈ 0.10-0.14; कोई हाइड्रोजन जोखिम नहीं | हाँ | ऑटोमोटिव, पवन ऊर्जा, उच्च शक्ति बोल्ट |
| जिंक-निकेल मिश्र धातु चढ़ाना | 500-1,500 घंटे | 8-15μm | μ ≈ 0.12–0.16; अच्छी स्थिरता | हाँ | ऑटोमोटिव अंडर-हुड, चेसिस |
| फॉस्फेट + तेल | 24-72 घंटे (केवल इनडोर) | 3-15μm | उत्कृष्ट - μ ≈ 0.12-0.14 | हाँ | इंजन आंतरिक, बंदूक घटक |
| ब्लैक ऑक्साइड | न्यूनतम (4-8 घंटे) | <1 μm | अच्छा; सजावटी | हाँ | उपस्थिति-महत्वपूर्ण, इनडोर उपकरण |
अभ्यास में नमक स्प्रे प्रदर्शन
एक यूरोपीय निर्माण उपकरण OEM ने हाल ही में अपनी फास्टनर आपूर्ति श्रृंखला का परीक्षण किया और पता लगाया कि मानक इलेक्ट्रोगैल्वेनाइज्ड बोल्ट ऑन व्हील लोडर एक्सेस पैनल्स नॉर्डिक सर्दियों की स्थिति (रोड नमक एक्सपोजर) में 18 महीने में विफल रहे थे। जियोमेट 500 जिंक फ्लेक कोटिंग के लिए स्विच - लगभग $0.012 प्रति M12 बोल्ट की वृद्धिशील लागत पर - तीन साल की अवलोकन अवधि में फास्टनर जंग से संबंधित वारंटी दावों को समाप्त कर दिया।.
इंजीनियरों को निर्दिष्ट करने के लिए कार्बन स्टील [[0] बाहरी अनुप्रयोगों में, अंगूठे का नियम स्पष्ट है: जस्ता चढ़ाना zफैक्ट्री फर्श उपकरण के लिए है; जस्ता फ्लेक या हॉट-डुबकी गैल्वनाइजिंग बारिश को देखने वाली किसी भी चीज़ के लिए है।.
हाइड्रोजन भ्रूण: तंत्र, जोखिम परिदृश्य और रोकथाम
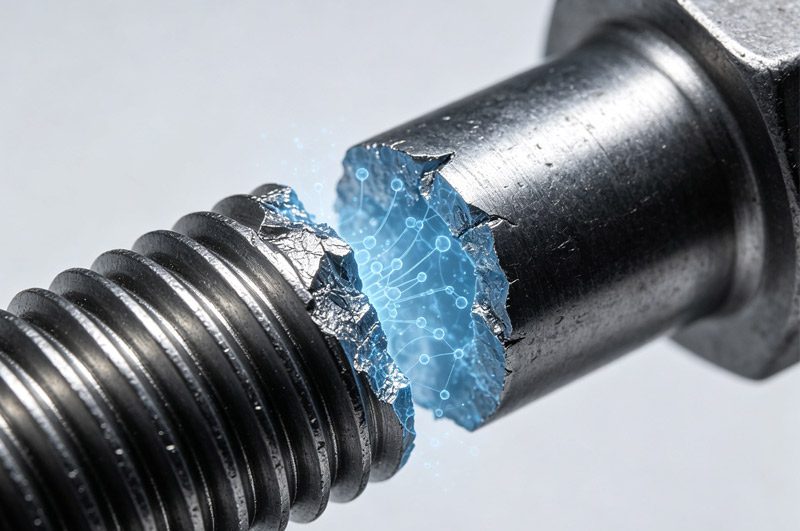
Hydrogen embrittlement (HE) is the silent failure mode that terrifies engineers working with high-strength कार्बन स्टील [[0]. The mechanism is insidious: atomic hydrogen diffuses into the steel lattice, accumulates at grain boundaries and stress concentrations, and causes sudden brittle fracture — often days or weeks after installation, at loads well below the bolt’s rated capacity.
How Hydrogen Enters the Steel
There are three primary ingress paths:
| Ingress Path | तंत्र | Risk Level for कार्बन स्टील [[0] |
|---|---|---|
| Electroplating | Cathodic hydrogen evolution during acid pickling and electroplating processes | उच्च — especially for hardness ≥ 32 HRC (ISO 898-1 Class 10.9 and above) |
| Service Environment | Cathodic protection systems, acidic process fluids | Moderate — more relevant to petrochemical and marine environments |
| विनिर्माण | Steelmaking moisture, wire drawing lubricant decomposition | Low — typically diffuses out during subsequent heat treatment |
Risk Thresholds and Susceptibility
The industry consensus, codified in ISO 15330 और ASTM F1940, establishes a clear hardness threshold:
Below 32 HRC (~1,050 MPa tensile) : Low susceptibility — hydrogen bake-out is generally not required
32–39 HRC (Class 10.9) : Moderate susceptibility — post-plating bake-out mandatory (typically 190–210°C for 4–8 hours within 1 hour of plating)
Above 39 HRC (Class 12.9) : High susceptibility — bake-out mandatory; some OEM specifications prohibit electroplating altogether in favor of zinc flake coatings
Prevention Strategies
The most robust approach is a multi-barrier strategy:
Process substitution : Where design permits, specify mechanical zinc plating or zinc flake coating (Geomet, Dacromet) instead of electroplating. These processes introduce negligible hydrogen.
Bake-out protocol : When electroplating cannot be avoided, enforce a documented bake-out cycle per ISO 9588: 190–210°C, 4 hours minimum for Class 10.9, 8 hours minimum for Class 12.9. The clock starts within 1 hour of removal from the plating bath.
सामग्री चयन : For fasteners in hydrogen-charging service environments, consider specifying ASTM A193 B7 (a chromium-molybdenum alloy steel) rather than carbon steel. The alloying elements improve resistance to hydrogen-induced cracking.
Design practices : Reduce notch sensitivity by specifying generous fillet radii at the head-to-shank transition and rolled threads (not cut threads), which introduce compressive residual stresses at the thread root.
Real-World Failure: Wind Turbine Tower Bolts
In 2018, a North American wind farm operator reported multiple bolt fractures at tower flange connections within 12 months of commissioning. The fasteners were ISO 898-1 Class 10.9 electrogalvanized M36 bolts. Failure analysis confirmed hydrogen embrittlement as the root cause. The corrective action — switching to zinc flake coating with documented bake-out — resolved the issue at a per-turbine cost increase of approximately $180, representing less than 0.02% of a turbine’s total installed cost.
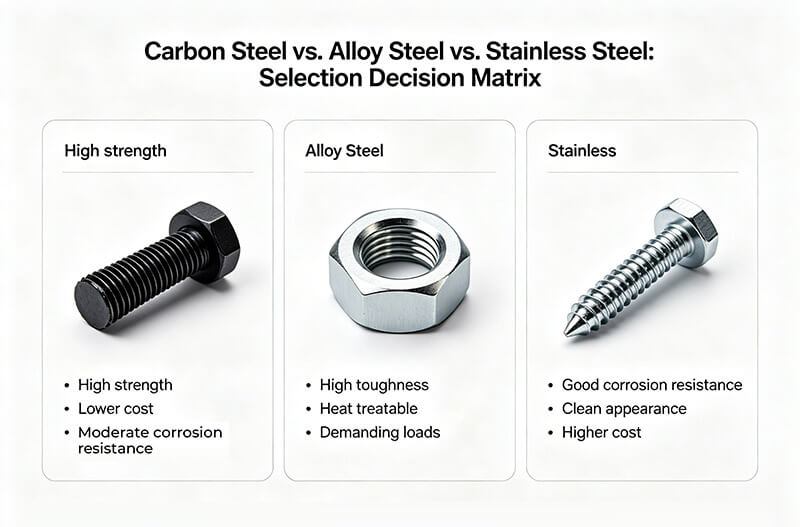
Carbon Steel vs. Alloy Steel vs. Stainless Steel: Selection Decision Matrix
OEM engineers routinely face the “which material?” question at the design review stage. The table below provides a structured comparison across the dimensions that matter most in procurement-driven decisions.
| Selection Criterion | Carbon Steel (C1045, Class 8.8) | Alloy Steel (SCM435, Class 10.9/12.9) | Stainless Steel (A2-70 / A4-80) |
|---|---|---|---|
| Base Material Cost (Index) | 1.0 | 1.8–2.5 | 4.0–6.0 |
| Achievable Tensile Strength | 800–1,000 MPa | 1,000–1,400 MPa | 500-800 एमपीए |
| जंग प्रतिरोध | Requires coating | Moderate (Cr-Mo content) | उत्कृष्ट |
| Low-Temperature Toughness | Fair — brittle below −20°C | Good — usable to −50°C with correct grade | उत्कृष्ट |
| High-Temperature Strength | Poor above 250°C | Good to 400–500°C | Good to 600°C+ |
| Hydrogen Embrittlement Risk | Moderate at Class 10.9+ | Lower (alloying improves resistance) | कम |
| Magnetic Properties | फेरोमैग्नेटिक | फेरोमैग्नेटिक | Austenitic grades (A2/A4): non-magnetic |
| Recyclability | 100% | 100% | 100% |
| Lead Time for Custom Parts | Shortest | मध्यम | Longest |
When Carbon Steel Is the Right Choice
Total installed cost is the primary constraint and the application environment is controlled (indoor, dry, or coated).
Tensile requirements fall within 400–1,000 MPa — the sweet spot where carbon steel delivers without the alloying premium.
The assembly process involves high-volume automated torquing where consistent friction coefficients matter — zinc flake-coated carbon steel excels here.
The design does not involve sustained elevated temperatures above 200°C.
When to Upgrade to Alloy or Stainless
Cyclic fatigue loading at stress amplitudes exceeding 50% of yield strength — alloy steel’s better hardenability provides more uniform cross-sectional properties in larger diameters.
Service temperature excursions above 250°C — carbon steel’s tempered martensite will continue to soften.
Corrosive environments where coating failure would be catastrophic — food processing, marine, chemical processing plants.
RoHS and REACH Compliance for कार्बन स्टील [[0]
European OEMs operating under the RoHS Directive 2011/65/EU और REACH Regulation (EC 1907/2006) impose strict substance restrictions on every component entering their supply chain — including कार्बन स्टील [[0].
RoHS Compliance Checklist for Carbon Steel Fasteners
| Substance | Limit (% by weight in homogeneous material) | Carbon Steel Relevance | Compliance Strategy |
|---|---|---|---|
| Lead (Pb) | 0.1% | Relevant to free-machining steel grades (e.g., 12L14) containing lead as machinability additive | Avoid specifying leaded free-machining grades for EU-bound fasteners |
| Mercury (Hg) | 0.1% | Negligible in carbon steel | Not applicable |
| Cadmium (Cd) | 0.01% | Historically used in plating; now rare | Prohibit cadmium plating; specify zinc or zinc flake alternatives |
| Hexavalent Chromium (Cr⁶⁺) | 0.1% | Highly relevant — Cr⁶⁺ passivation was standard in zinc plating for decades | Mandate trivalent chromium (Cr³⁺) passivation per REACH Annex XVII Entry 47 |
| PBB / PBDE (flame retardants) | 0.1% | Not relevant to steel | Not applicable |
| DEHP / BBP / DBP / DIBP (phthalates) | 0.1% | May be present in thread-locking patch materials (nylon) | Specify RoHS-compliant pre-applied thread lockers (e.g., Loctite Dri-Loc series) |
The Hexavalent Chromium Sunset
Hexavalent chromium passivation — the “yellow zinc” finish familiar to every hardware buyer — has been effectively banned for most industrial applications in the EU since September 2017 under REACH Annex XVII (Entry 47 sunset date). Trivalent chromium passivation (Cr³⁺) has become the default replacement, offering comparable corrosion resistance with a silver-white or blue-tinted appearance.
For engineers writing procurement specifications, the correct call-out is critical. Instead of the legacy “Zinc Plated per ASTM B633, Type III” (which historically implied yellow hexavalent chromate), specify:
“Zinc electroplated per ASTM B633, Type V (trivalent chromium passivate), Fe/Zn 5AN per ISO 4042.”
REACH Substances of Very High Concern (SVHC) Monitoring
Carbon steel itself — iron with less than 2% carbon — is not an SVHC candidate. However, supply chain transparency matters. European OEMs increasingly require full material declarations (FMD) under the IMDS (International Material Data System) framework. A responsible fastener supplier provides:
Mill test certificates (EN 10204 Type 3.1) for each heat of steel
Surface treatment chemistry declarations identifying all process chemicals
REACH SVHC compliance statement updated to the latest candidate list (currently 241 substances as of January 2026)
Chinese Grade to International Standard Cross-Reference
Many equipment OEMs source कार्बन स्टील [[0] from Chinese manufacturers. Understanding the equivalence — and the gaps — between GB (Chinese national standards) and international systems is essential for quality assurance.
Carbon Steel for Fasteners: GB to ASTM / ISO / EN / DIN Cross-Reference
| GB/T Grade | Carbon Content Range | Closest ASTM | Closest ISO 898-1 | Closest EN | Closest DIN | नोट्स |
|---|---|---|---|---|---|---|
| Q235 (GB/T 700) | 0.14–0.22% | ASTM A307 Gr. A | Class 4.6 | EN 10263-1 C4C | DIN 1.0301 | General structural; not for heat-treated fasteners |
| ML08Al (GB/T 6478) | ≤ 0.10% | — | Class 4.8 (cold-heading) | EN 10263-2 C2C | — | Aluminum-killed low-carbon cold-heading steel |
| ML35 (GB/T 6478) | 0.32–0.39% | SAE J429 Gr. 5 | कक्षा 8.8 | EN 10263-3 C35 | DIN 1.1181 | Medium-carbon cold-heading quality |
| ML40Cr (GB/T 6478) | 0.38–0.45% (+Cr) | SAE J429 Gr. 8 | कक्षा 10.9 | EN 10263-4 34Cr4 | DIN 1.7033 | Alloy cold-heading steel; technically alloy steel, not plain carbon |
| SWRCH35K (JIS-derived) | 0.32–0.38% | SAE J429 Gr. 5 | कक्षा 8.8 | — | — | Cold-heading wire rod; widely used in Asia-Pacific fastener production |
| SWRCH45K (JIS-derived) | 0.42–0.48% | ASTM A325 Type 1 | कक्षा 10.9 | — | — | Medium-carbon; suitable for quench-and-temper |
| C1035 (GB/T 699) | 0.32–0.38% | ASTM A29 1035 | कक्षा 8.8 | EN 10083-2 C35 | DIN 1.0501 | Direct equivalent across GB/ISO/EN systems |
| C1045 (GB/T 699) | 0.43–0.50% | ASTM A29 1045 | कक्षा 10.9 | EN 10083-2 C45 | DIN 1.0503 | Direct equivalent across GB/ISO/EN systems |
Critical Equivalence Gaps to Watch
Three areas require particular scrutiny when qualifying Chinese-supplied carbon steel fasteners against international specifications:
Phosphorus and Sulfur limits : GB/T standards historically permitted slightly higher P and S ceilings (0.035–0.040%) than some ASTM specifications (0.030% max for certain grades). For critical applications, specify “GB/T 699 high-quality structural carbon steel” which tightens the limits.
Decarburization : Thread decarburization is the most common non-conformance found in third-party inspection of imported fasteners. Specify “no complete decarburization, partial decarburization depth ≤ 1.5% of thread pitch” and require micro-hardness traverse testing per ISO 898-1 Annex B.
Traceability : EN 10204 Type 3.1 certification is not universally standard practice in all Chinese mills. It must be explicitly requested in the purchase order for EU-bound shipments.
Real-World OEM Case Studies
Case 1: Agricultural Equipment Manufacturer — Grade Migration to Reduce Cost
Context : A Midwestern US manufacturer of combine harvesters had been specifying SAE J429 Grade 8 (alloy steel, quenched and tempered) bolts for non-critical chassis panel attachments — over 180 fasteners per machine, 22,000 machines annually.
Challenge : The engineering team conducted a joint-by-joint load analysis and identified 140 of the 180 locations where the actual clamp load requirement was below 60% of an SAE J429 Grade 5 (medium-carbon steel, C1035 equivalent) bolt’s proof load.
Solution : The 140 locations were downgraded from Grade 8 (alloy steel) to Grade 5 (C1035 carbon steel) with Geomet 500 zinc flake coating. The remaining 40 locations at high-stress engine mount and axle connections retained Grade 8.
परिणाम : Annual fastener cost reduction of $187,000 — a 38% decrease — with zero field failures attributable to the grade migration over a two-year monitoring period.
Key Takeaway : कार्बन स्टील [[0] are not a compromise; they are the correct material when the application’s load requirements are well-matched to the grade.
Case 2: European Energy Storage OEM — Hydrogen Embrittlement Elimination
Context : A German manufacturer of utility-scale battery energy storage system (BESS) enclosures experienced in-field bolt fractures on outdoor cabinet door hinges after 8 months in a North Sea coastal installation.
Challenge : The M8 socket head cap screws were ISO 898-1 Class 12.9, electrogalvanized (zinc-plated). Failure analysis at an independent German laboratory (MPA Stuttgart) confirmed hydrogen-induced stress corrosion cracking. The coastal chloride environment accelerated crack propagation after hydrogen had been introduced during electroplating.
Solution : The specification was revised to:
Downgrade from Class 12.9 to Class 10.9 (reducing hardness from 42 HRC to 36 HRC — below the HE danger zone)
Switch from electrogalvanized to Geomet 321 zinc flake coating
Mandate a documented bake-out protocol per ISO 9588 (200°C, 4 hours)
परिणाम : Zero fractures reported across 1,200 cabinets over a subsequent 24-month monitoring period. The material cost change was neutral — the coating cost increase was offset by the lower base material cost of Class 10.9 vs. 12.9.
Key Takeaway : Hydrogen embrittlement prevention is a systems problem requiring coordinated decisions across grade selection, coating specification, and process control.
Case 3: Italian Rail Component Supplier — Surface Finish Optimization for Automated Assembly
Context : A Northern Italian Tier-1 supplier of railway interior components (seat frames, luggage racks, partition panels) operates fully automated assembly cells with multi-spindle torque tools.
Challenge : The automated cells experienced a 4.2% rejection rate due to torque-angle monitoring alarms — some joints fell outside the ±15% target torque window. Root cause analysis identified inconsistent friction coefficients (μ = 0.09 to 0.19) on electrogalvanized M10 carbon steel bolts from the incumbent supplier.
Solution : The supplier was required to switch to a zinc flake coating (Geomet 500) with an integrated topcoat lubricant that delivers a controlled coefficient of friction of μ = 0.12 ± 0.02. The specification now reads: “Zinc flake coating per ISO 10683 with integral lubricant; coefficient of friction μ = 0.10–0.14 per ISO 16047.”
परिणाम : Torque rejection rate dropped to 0.3%. Annual rework cost savings of approximately €94,000. The assembly line throughput increased 2.1% due to reduced station stoppages.
Key Takeaway : Fastener surface finish is a hidden variable in automated production economics. A few cents per bolt in finishing cost can return orders of magnitude more through reduced assembly rework.
अक्सर पूछे जाने वाले प्रश्न
Q: What is the difference between C1035 and C1045 for fastener production?
A: The primary difference is carbon content — C1035 contains 0.32–0.38% carbon, while C1045 contains 0.43–0.50%. This translates to a higher achievable hardness and tensile strength for C1045 after quenching and tempering (typically 800–1,000 MPa vs. 700–900 MPa for C1035 under comparable heat treatment). However, C1045 is more prone to quench cracking in complex geometries. For ISO Class 8.8 bolts, C1035 is almost always sufficient. C1045 is normally reserved for Class 10.9 fasteners.
Q: Can कार्बन स्टील [[0] be used outdoors?
A: Yes — with the correct surface protection. Uncoated carbon steel will rust within days of outdoor exposure. Hot-dip galvanizing (per ASTM A153 or ISO 10684) or zinc flake coating (per ISO 10683) can provide 15–30 years of outdoor service life in non-marine environments. The key is matching the coating system to the expected corrosivity category (ISO 9223 C1 through C5).
Q: Are carbon steel bolts magnetic?
A: Yes. All carbon steels are ferromagnetic. This can be an advantage or disadvantage depending on the application. MRI equipment and certain sensor assemblies require non-magnetic fasteners (austenitic stainless steel A2/A4). Conversely, magnetic carbon steel fasteners are useful in automated assembly where magnetic bit-holding is needed.
Q: What is the maximum recommended service temperature for carbon steel fasteners?
A: Tempered carbon steel fasteners begin to lose strength at sustained temperatures above approximately 200°C, as the tempering process effectively continues in service. For applications above 250°C, alloy steels containing chromium and molybdenum (such as ASTM A193 Grade B7 or B16) are strongly recommended.
Q: How do I verify that a Chinese supplier’s carbon steel meets my specification?
A: Require three documents as a minimum package: (1) EN 10204 Type 3.1 mill test certificate for each heat, (2) an ISO 17025-accredited third-party test report covering chemical composition, tensile properties, and hardness on a sample from the shipment lot, and (3) a surface treatment certificate of conformance listing the process chemistry and salt spray test results. For critical applications, specify thread decarburization micro-hardness testing per ISO 898-1 Annex B.
Q: Does RoHS apply to carbon steel fasteners?
A: Carbon steel itself is RoHS-compliant. The compliance risk lies in the surface treatment — specifically, hexavalent chromium (Cr⁶⁺) passivation, which is restricted under both RoHS and REACH. Always specify trivalent chromium (Cr³⁺) passivation for zinc-plated fasteners destined for the EU market. Additionally, avoid free-machining carbon steel grades containing lead (e.g., 12L14) for EU shipments.
Q: What is boron-treated carbon steel (10B21), and when should I use it?
A: 10B21 is a low-carbon steel (0.18–0.23% C) microalloyed with a small addition of boron (5–30 ppm). Boron dramatically increases hardenability, allowing 10B21 to achieve mechanical properties comparable to medium-carbon C1045 after quenching and tempering — while retaining the superior cold formability of low-carbon steel. It is particularly well-suited for complex cold-headed geometries (flange bolts, special-head fasteners) that would crack if formed from C1045 wire. 10B21 is widely used in automotive fasteners and is a cost-competitive alternative for Class 10.9 bolts.
Conclusion
कार्बन स्टील [[0] are not an afterthought in the OEM parts bin. They are an engineered component whose performance depends on an interlocking chain of decisions: carbon content → heat treatment parameters → surface finishing chemistry → quality verification. Get any link wrong, and the consequences range from nuisance corrosion to catastrophic brittle fracture.
Guxiang Metalwork specializes in custom कार्बन स्टील [[0] for equipment OEMs — from prototype development through annual frame contracts. If you have a drawing or specification you would like quoted, submit it through our inquiry form for a response within 24 hours.